
Bucket on wheels
Well-known member
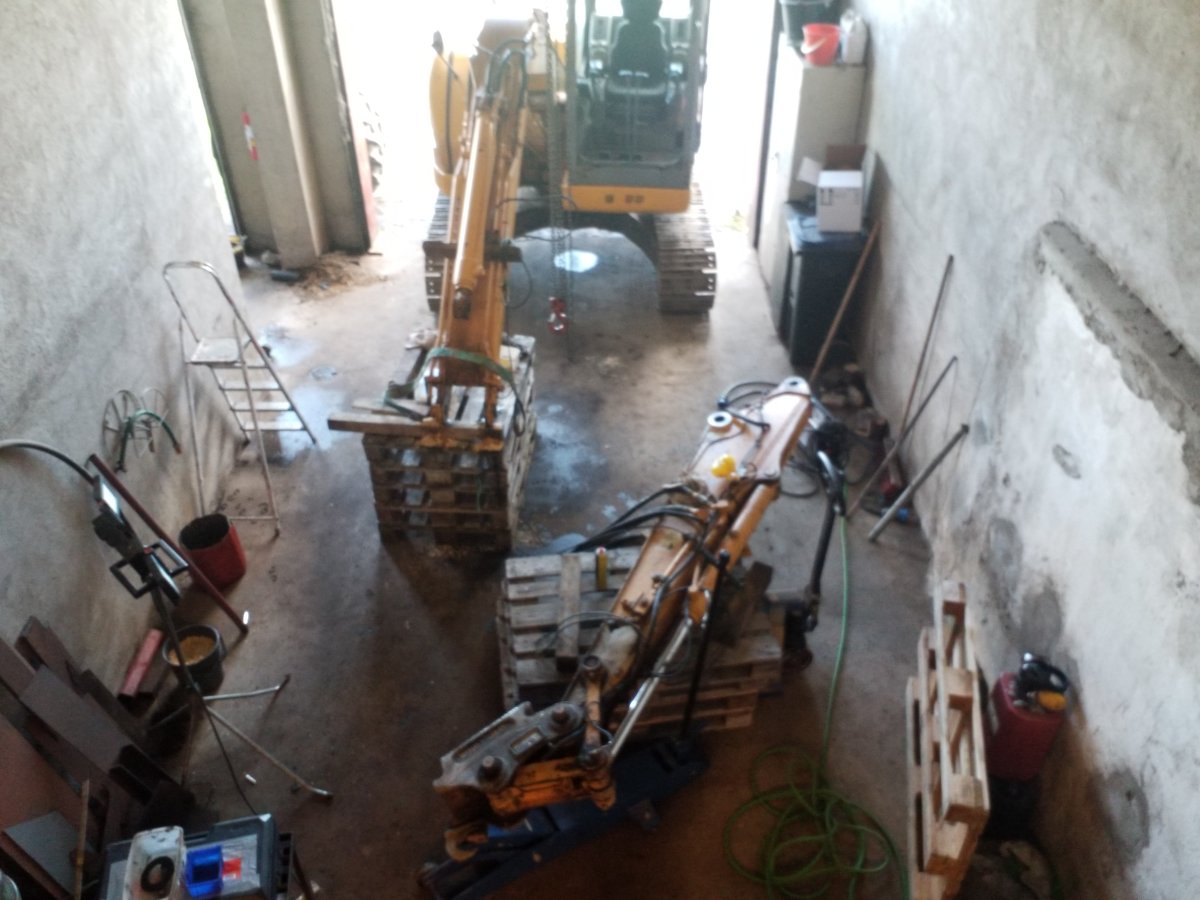
A friend of mine has this Kato 308 that has cracked along the side of the weld where the dipper bolt goes through.
After gulching with the plasma. I found that the crack goes through both plates. Any thoughts of how to fix this, and make it so strong that it will not crack again. At my disposal, I have a
Hyperterm 45XP. plasma burner. And a reasonably strong mig. welder. with 1.2 mm tube wire
Does the welding joint I've burned out look reasonable or should it be shaped differently ?
and how should I go along welding this backed up ?
Welding in straight strings or pendulum motion
My plan so far is to weld a straight string at the bottom. Then pendulum motion until I have filled up the welding joint.
Then grind the weld flat.
And then weld on a 10 mm plate.
That's a little smaller, at the shape of the original strengthening plate.
Any advice how to perform this is welcome.
So what you're saying V8druid ?
Are my attack on this ?
On the crazy side or the right side ?
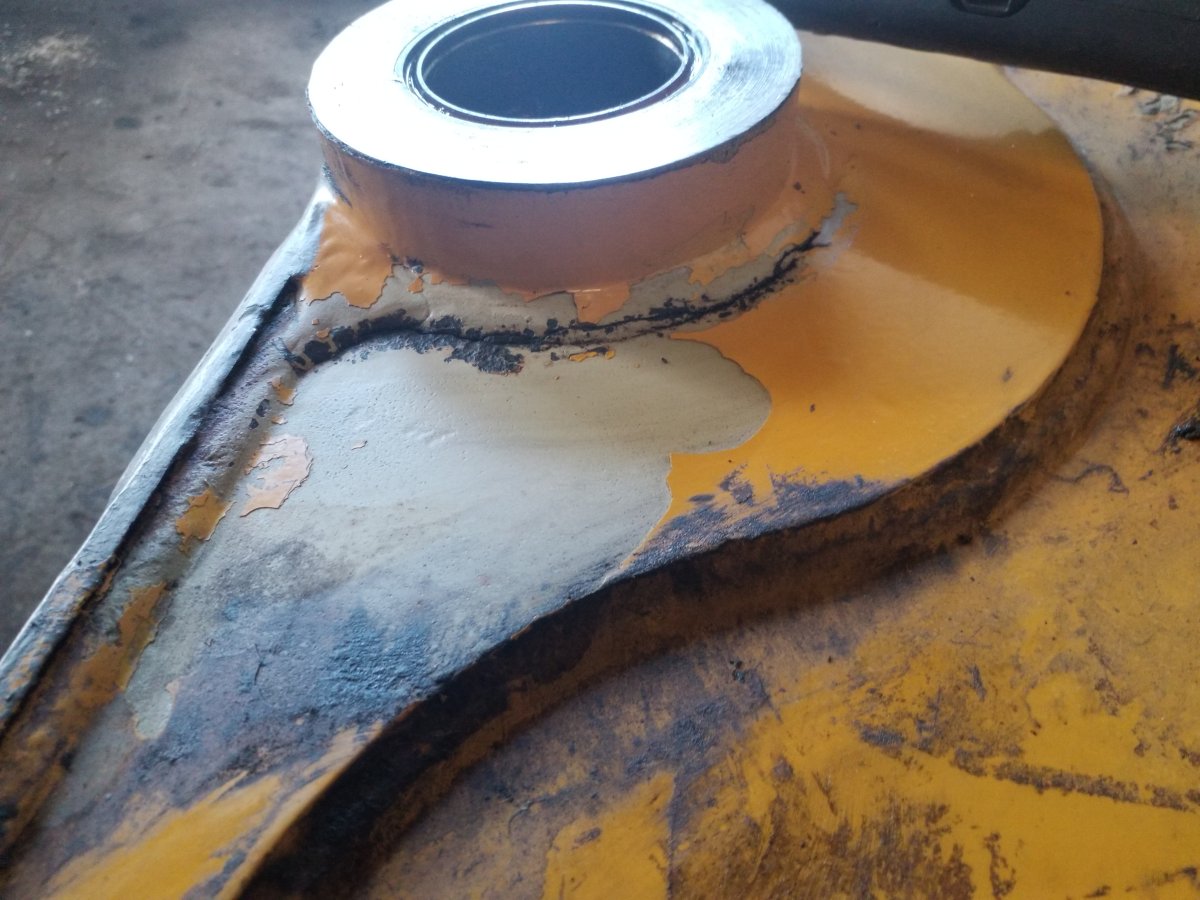
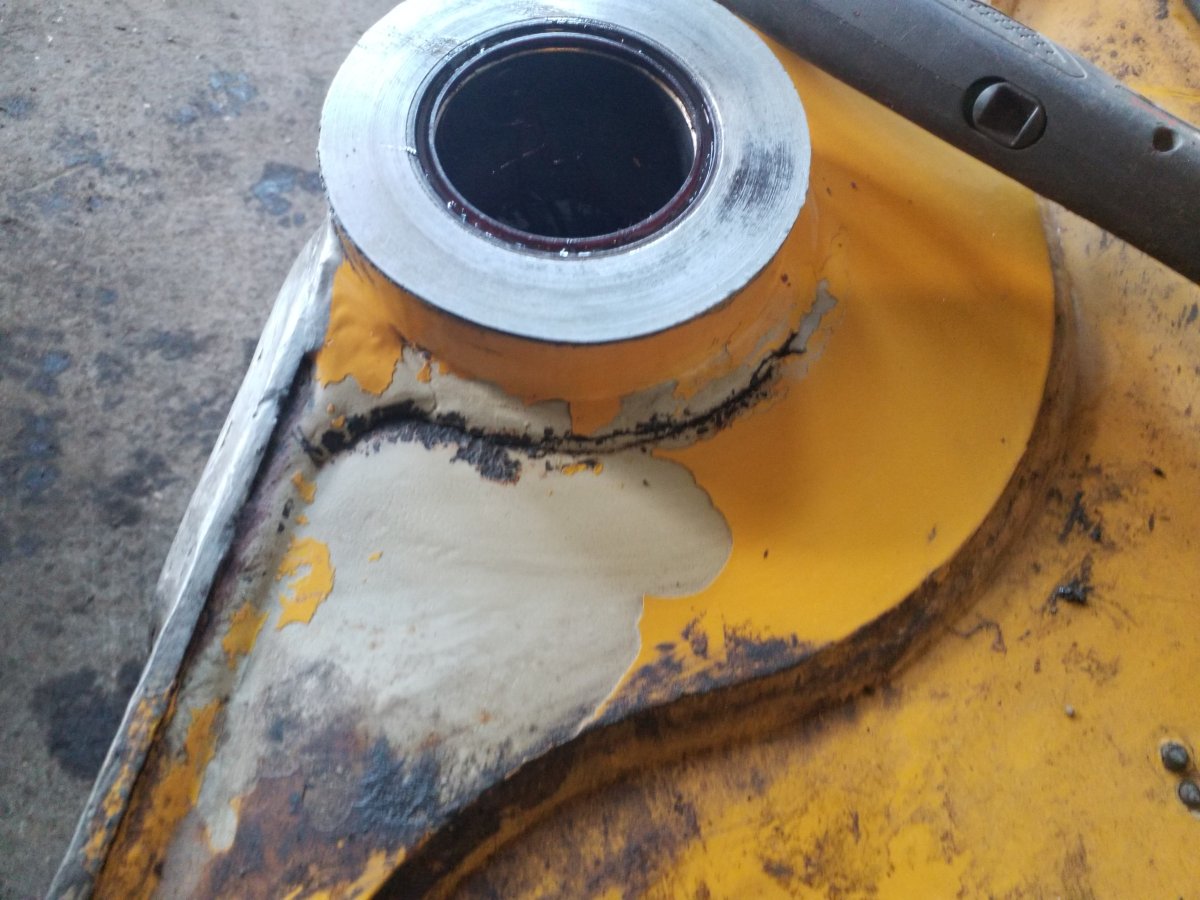
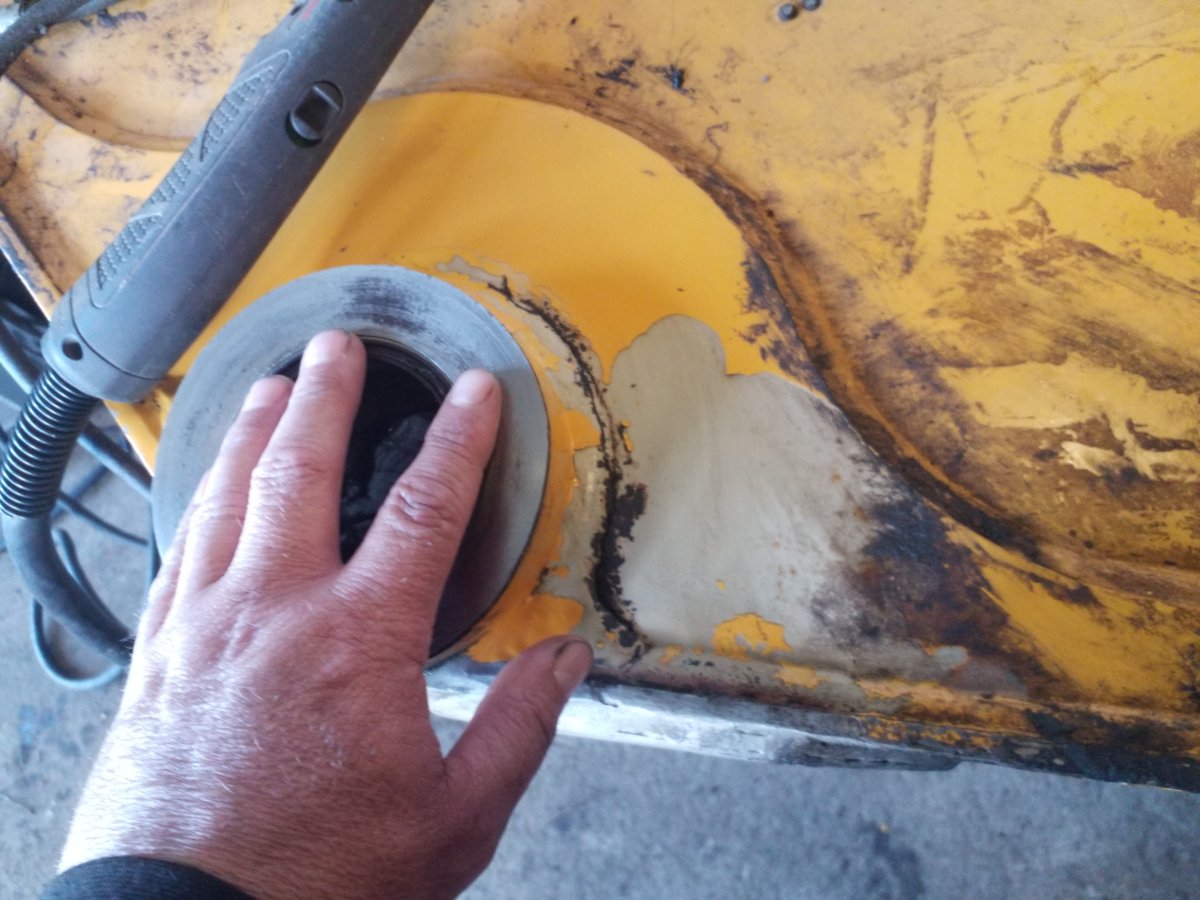
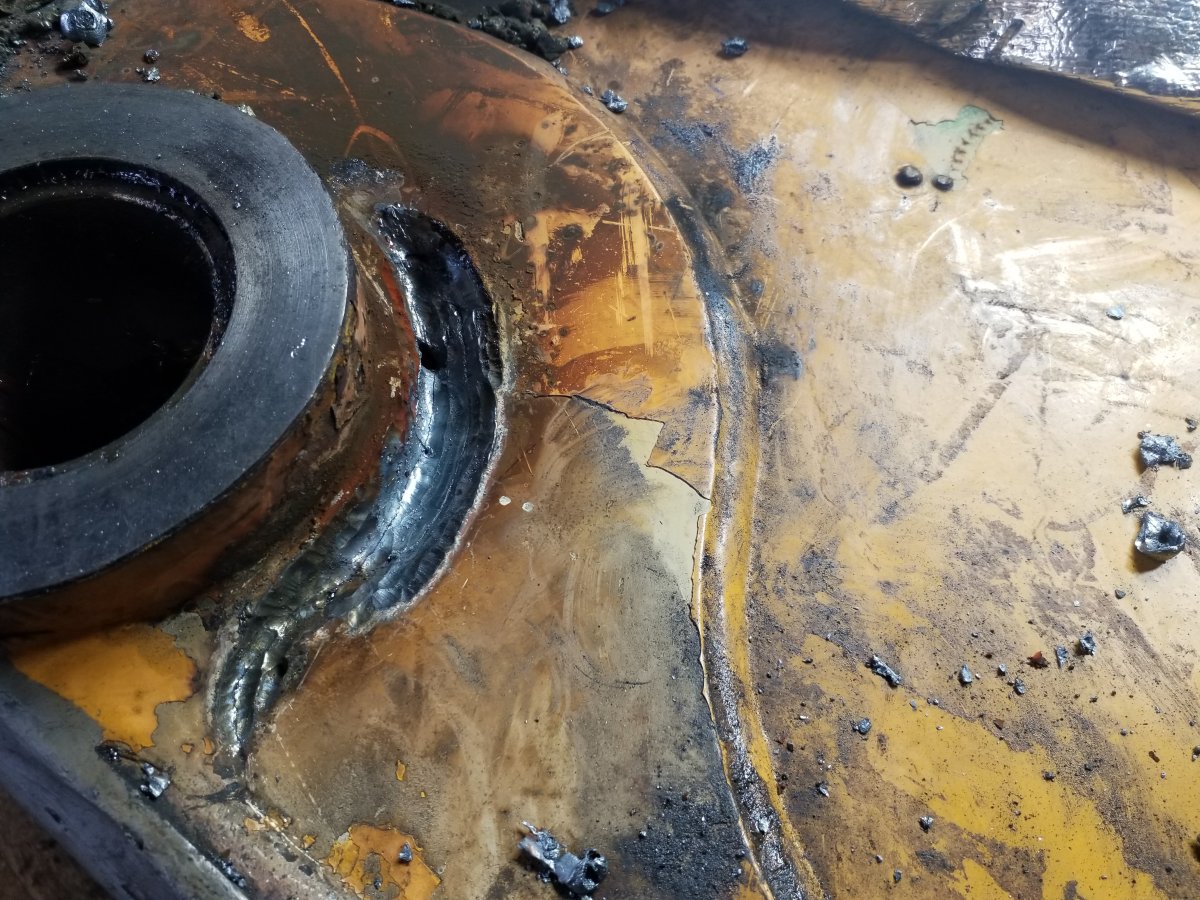
I'm not finished gouging on the the right part of the crack.
I stopped gouging when the big dipper bolt pipe reached a temperature of 200 C
A Continuously measured the temp with a infrared temp gauge
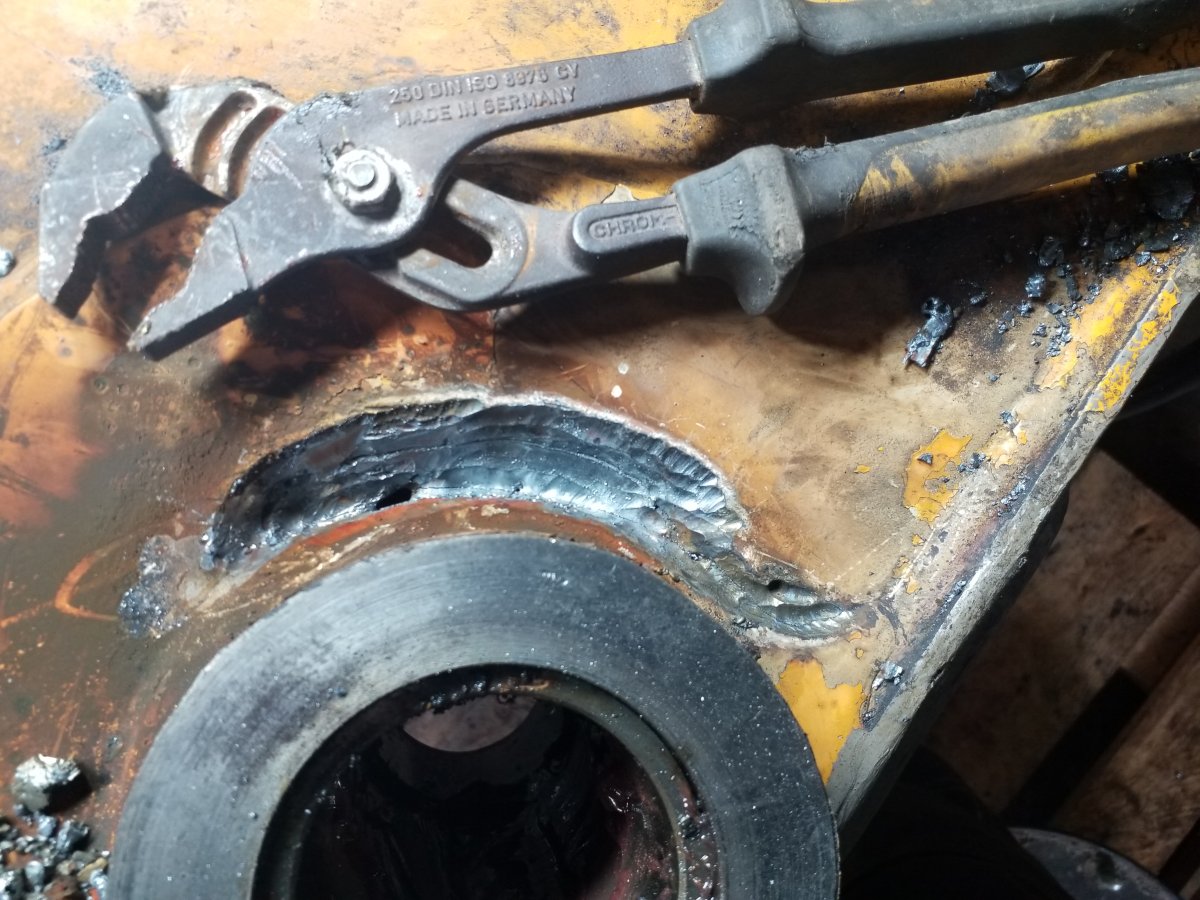
After gulching with the plasma. I found that the crack goes through both plates. Any thoughts of how to fix this, and make it so strong that it will not crack again. At my disposal, I have a
Hyperterm 45XP. plasma burner. And a reasonably strong mig. welder. with 1.2 mm tube wire
Does the welding joint I've burned out look reasonable or should it be shaped differently ?
and how should I go along welding this backed up ?
Welding in straight strings or pendulum motion
My plan so far is to weld a straight string at the bottom. Then pendulum motion until I have filled up the welding joint.
Then grind the weld flat.
And then weld on a 10 mm plate.
That's a little smaller, at the shape of the original strengthening plate.
Any advice how to perform this is welcome.
So what you're saying V8druid ?
Are my attack on this ?
On the crazy side or the right side ?
I'm not finished gouging on the the right part of the crack.
I stopped gouging when the big dipper bolt pipe reached a temperature of 200 C
A Continuously measured the temp with a infrared temp gauge


